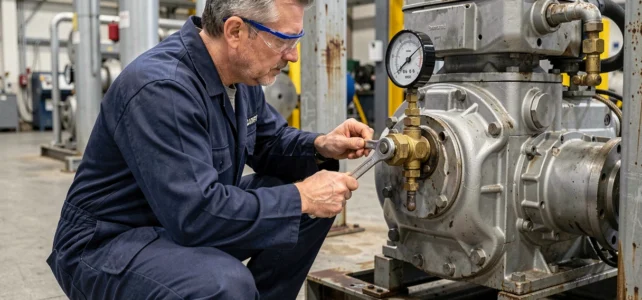
A hydraulic pump that vibrates, a cylinder that slows down for no reason, a relief valve that whistles: these symptoms often point to a poorly calibrated pressure setting. Adjusting the pressure of a hydraulic pump is not just about turning a screw on a limiter. It involves several parameters related to the circuit, the fluid, and the measuring instruments.
Trapped air and degassing: the cause of drift that the pressure gauge does not show
Have you ever noticed a pressure that fluctuates by a few bars without explanation? Trapped air in the circuit is often responsible. An air bubble compressed in a pipe behaves like a spring: it absorbs and then releases energy unpredictably.
The problem is that this instability skews the setting. You adjust the pressure limiter thinking you have found the right value, but the reading fluctuates as soon as the flow changes. Bleeding the air from the high points of the circuit before any adjustment is the first concrete step.
Degassing involves bleed valves positioned at the tops of the pipes and at the reservoir level. A reservoir that is too small or poorly baffled promotes the re-aspiration of air through the strainer. If the hydraulic fluid foams on the surface in the reservoir, it is a direct sign of excessive aeration. As long as this problem persists, any pressure adjustment remains approximate.
The detailed techniques for adjusting hydraulic pressure on Android Inside also cover this preliminary purging step, which conditions the reliability of the entire process.
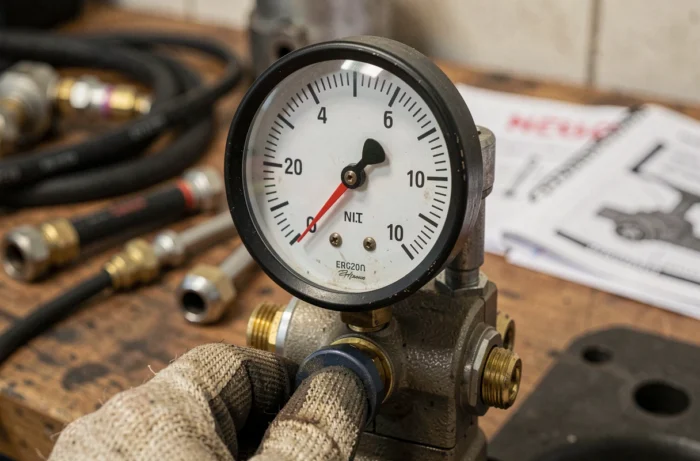
Pressure measurement point: where to place the sensor changes everything
An adjustment may seem correct on the pump’s pressure gauge yet prove ineffective at the cylinder or hydraulic motor level. The reason lies in the pressure losses in the circuit.
Between the pump outlet and the point of use, the fluid passes through distributors, hoses, and sometimes filters. Each component creates a pressure drop. Measuring the pressure at the manifold does not reflect the actual pressure at the cylinder.
Specifically, it is necessary to distinguish between two values:
- The pressure at the pump discharge, which indicates what the pump delivers to the circuit.
- The pressure at the point of use (cylinder inlet, motor), which represents the energy actually available for mechanical work.
- The difference between the two, which corresponds to the cumulative pressure losses in the pipes, fittings, and intermediate components.
If you adjust the pressure solely on the gauge at the pump outlet, you risk underfeeding the actuator. Placing a second measurement point near the working component allows you to verify that the useful pressure matches the actual need.
Calibration of the gauge and hysteresis control
The pressure gauge is the reference tool for adjustment. However, a gauge itself can drift. An instrument that displays an error of a few bars is enough to skew the entire process.
Calibrating the gauge before each adjustment campaign prevents working from an erroneous basis. Calibration involves comparing the instrument’s reading with a known reference and then correcting the deviation if necessary.
The hysteresis of the gauge is another trap. This term refers to the difference in reading between a pressure increase and a decrease. Specifically, if you increase to a certain pressure and then decrease, the needle may not return exactly to the same point. A gauge with too wide a hysteresis makes the adjustment non-repeatable.
How to check hysteresis in practice
Gradually increase the pressure to the target value and note the display. Slowly decrease and pass through the same value again. If the difference between the two readings exceeds the tolerance indicated by the gauge manufacturer, the instrument must be replaced or recalibrated.
Pressure adjustment on a variable frequency drive system
On circuits equipped with a variable frequency drive (VFD), pressure adjustment no longer goes through the classic limiter. The principle changes: instead of mechanically setting a maximum pressure, the speed of the electric motor is adjusted based on sensor feedback.
A pressure sensor sends a signal to the VFD controller. If the pressure drops below the setpoint, the VFD speeds up the motor. If it rises too much, it slows it down. This closed-loop operation offers finer regulation and reduces energy consumption.
The adjustment then incorporates pressure losses, altitude differences, and the most demanding area of the network. For example, in an irrigation circuit or an extensive industrial network, the furthest or highest point determines the minimum pressure setpoint. Adjusting below this deprives that area of sufficient flow.
NPSHa margin and minimum acceptable flow
With a VFD, the speed can drop very low. The risk: falling below the minimum acceptable flow of the pump. Below this threshold, the fluid no longer circulates enough to cool the bearings, and internal components overheat.
The margin between the available NPSH (NPSHa) and the required NPSH (NPSHr) of the pump must remain positive. If the VFD reduces the speed too much, this margin decreases, and cavitation occurs. Checking the minimum flow and NPSH margin protects the pump against premature wear.
Relief valve and pressure limiter: adjust without exceeding
The pressure limiter (or relief valve) protects the circuit against overpressure. Its adjustment is generally done by a screw that compresses an internal spring. Turning clockwise increases the setting pressure, while turning counterclockwise decreases it.
The reliable procedure follows a precise order:
- Completely loosen the adjustment screw to start from a low pressure.
- Put the system into operation and gradually increase the pressure by slowly tightening.
- Observe the calibrated gauge at the relevant measurement point and stop at the target value.
- Lock the locknut to fix the adjustment, then check a second time under load.
Never adjust the relief valve beyond the nominal pressure of the most fragile components in the circuit (hoses, fittings, seals). The limiter exists to protect the system, not to push its limits.
A reliable pressure adjustment therefore combines air purging, correct sensor positioning, instrument calibration, and adherence to the operating margins of the pump. Each skipped step introduces uncertainty that accumulates with others, leading to failures or accelerated wear of hydraulic components.